Top 10 Stationary Oven Carousel Rotomolding Machines for Reliable Production
2026-10-09
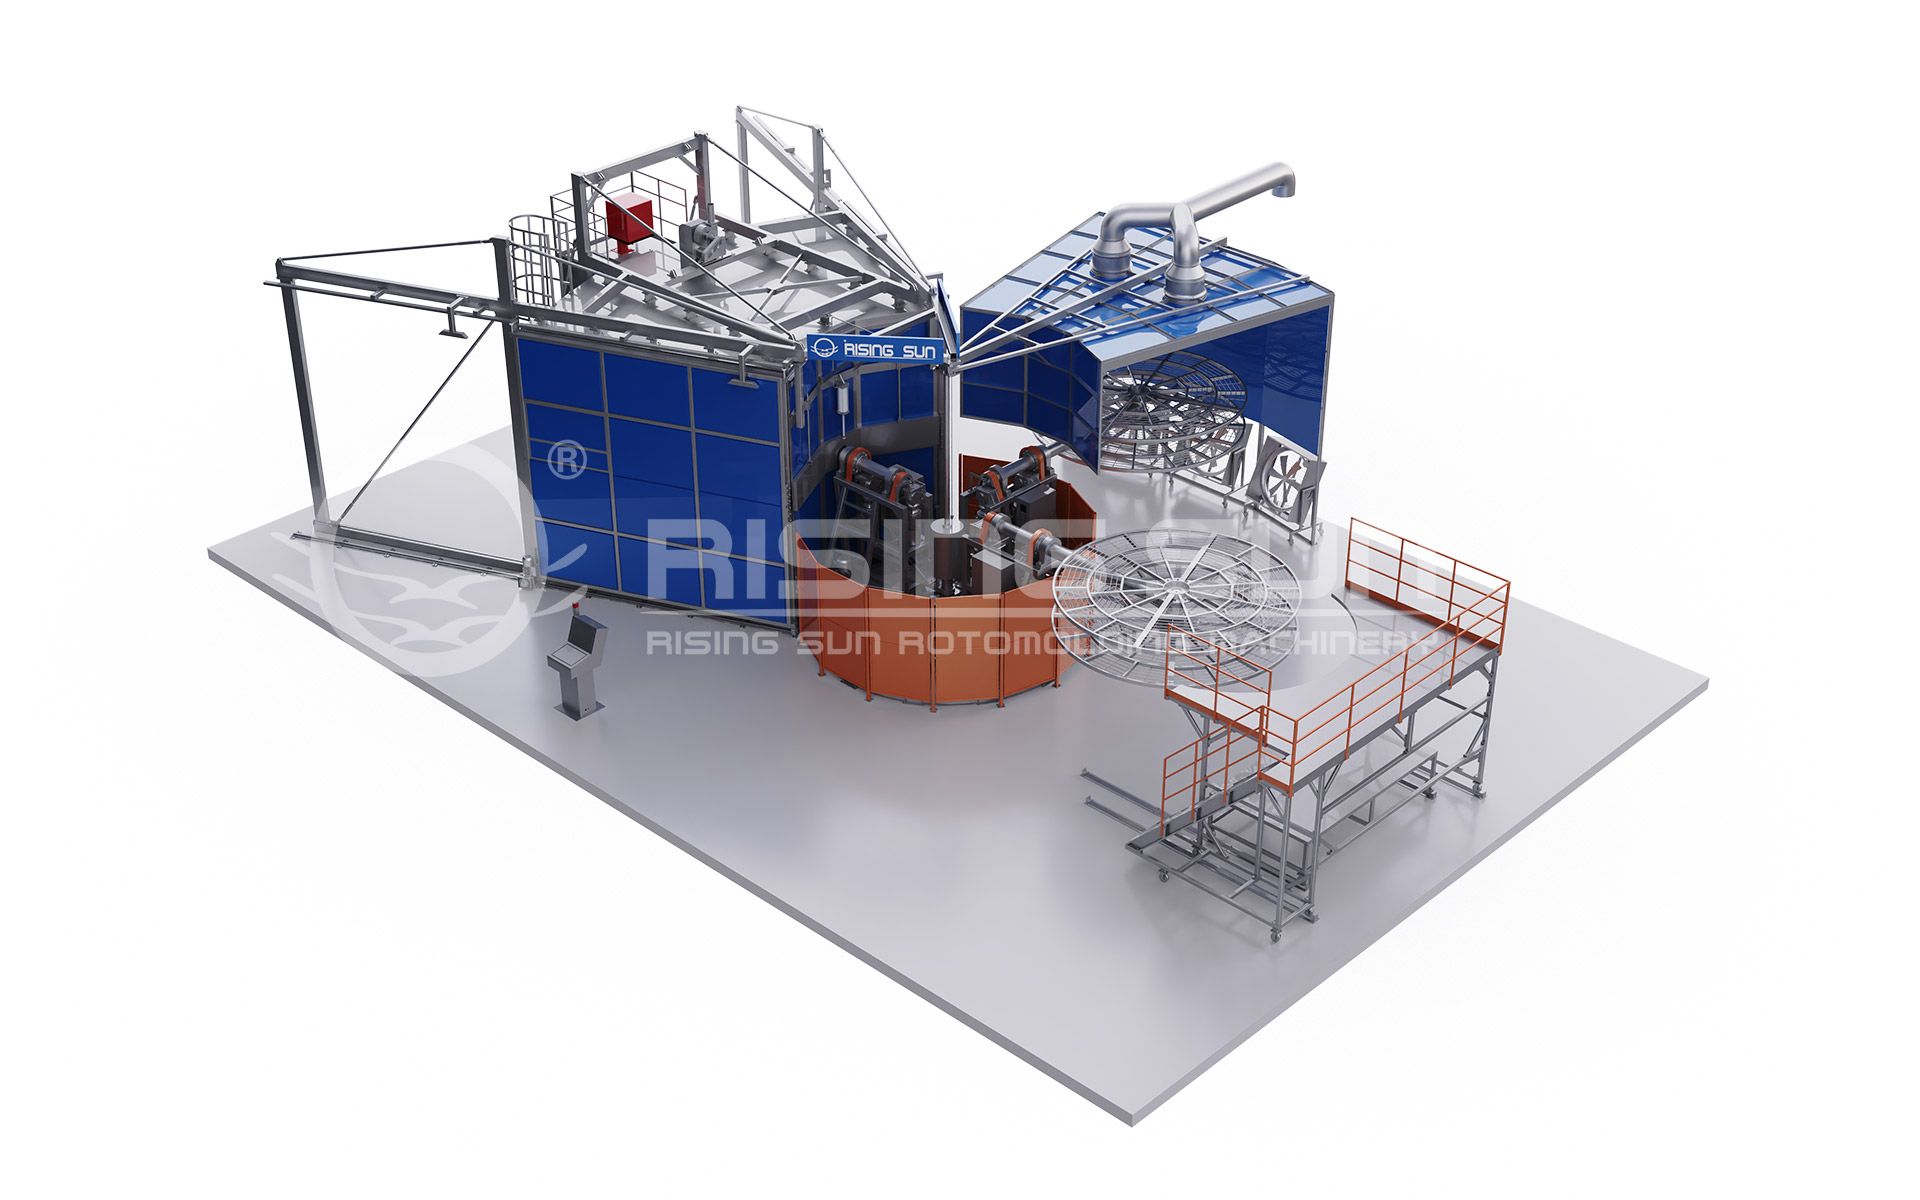
Rotomolding success rarely depends on a single factor, but the machine you choose can make or break your production schedule. Stationary oven carousel machines, in particular, are known for their balance of flexibility and repeatability — yet not all are built for true reliability. In this roundup of the top 10 stationary oven carousel rotomolding machines, we focus on models that actually hold up under real-world demand. Along the way, Rising Sun emerges as a name worth watching, thanks to a design philosophy that favors uptime over gimmicks.
What Makes Oven Airflow More Important Than Peak Temperature?
Most home cooks obsess over the dial number, but the real magic in your oven happens when hot air moves. A high peak temperature with dead, stagnant heat creates uneven patches—burnt edges on a tray of cookies, pale centers on a roast. Airflow evens out those wild swings, letting the same 400°F behave like a professional deck oven instead of a box with a heating coil.
Think about what actually browns food: convection, not just conduction. When air circulates, moisture escapes from surfaces faster, triggering the Maillard reaction at lower effective temperatures. A potato wedge in still air at 450°F may steam itself soft before it crisps, while a 400°F oven with strong airflow gives you shatteringly crisp skin. That’s why commercial combi ovens prioritize fan speed and baffle design over raw burner output.
Airflow also changes how you can load the oven. With weak circulation, you’re stuck with one tray in the middle, rotating halfway through, praying for consistency. Strong airflow lets you stack multiple racks, slide in a pizza steel or cast iron without wrecking the temperature recovery, and actually trust the dial. Peak temperature is a headline number; airflow is the invisible hand that makes every square inch of that number usable.
Independent Arm Drives: Where the Cycle Time Gains Actually Show Up
The biggest chunk of saved time rarely appears on the main stroke. It shows up in the small, awkward pauses between a vertical pick and a horizontal transfer—moments where a coupled system has to wait for both arms to settle. With independent drives, the lighter Z-axis can already be dropping toward the next part while the heavier X-axis is still finishing its deceleration ramp. That overlap often trims 0.3 to 0.6 seconds per cycle, and in a 24/7 automotive line that compounds into thousands of extra shots every month.
You also see the gains when running mixed molds or quick tool changes. An independent arm can be tuned with a stiffer jerk setting for short, precise insert loading, while the other arm runs a softer profile for bulky part removal. There is no need to compromise both motions around a shared torque budget. Operators tend to notice the difference not in cycle charts but in the steady rhythm of the discharge conveyor—fewer hesitations, fewer alarm stops for "axis not in position."
Finally, the benefit sticks over time. Coupled drives drift out of sync as belts wear, and re-syncing them often means shaving off the very cycle time you gained. Independent arms stay on their own servo loops, so a maintenance adjustment on one side does not force a re-teach of the other. That means the cycle time you captured during commissioning is still there in month fourteen, long after the initial gains have become the new baseline.
How Residual Stress Hides in Parts Pulled Too Early
When a part is ejected before the material has fully stabilized, the outer skin may look perfectly fine. But inside, polymer chains or metal grains are frozen in a strained configuration. The part carries a hidden tension—residual stress—that doesn't show up on the surface or in a quick dimensional check. It's like a coiled spring waiting for a trigger.
That trigger often arrives later, as heat, moisture, or a minor load. The part slowly warps, cracks, or loses tolerance without any obvious cause. Because the stress was locked in at the molecular or grain level during premature cooling, it can't be detected by eye or simple calipers. You only notice it after assembly or in the field.
To find it early, you need methods that look beneath the skin—hole-drilling, X-ray diffraction, or a simple solvent test for some plastics. But the better approach is prevention: respect the cooling time, keep ejection force low, and let the part stabilize before you measure or ship.
Gas, Electric, or Hybrid Heat: Which Choice Keeps Repeatability High?
Repeatability in a heated process rarely comes down to the energy source alone. It hinges on how tightly the system can return to the same temperature profile cycle after cycle. Electric elements respond almost instantly and can be pulsed rapidly, which supports a narrow temperature band—if the controller is good. Gas burners, by contrast, have a lag as the flame adjusts and the heat exchanger warms or cools, so the temperature tends to swing wider around the setpoint. Hybrid setups aim to borrow the best of both, but they add a changeover decision that must be tuned carefully.
Single-stage gas heat is often the weakest choice for repeatability because the burner is either full-on or full-off. Each cycle delivers a sharp burst of heat, then a long coast down, creating a sawtooth temperature pattern that varies slightly with ambient conditions. Electric resistance heat can dodge that problem through fast switching or phase-angle control, holding a steadier temperature with small, regular pulses. Inverter-driven heat pumps, a form of electric heat, go further by varying output over a wide range, so the system can settle into a near-continuous low-level input instead of cycling.
A hybrid system can actually beat both if the control logic is set up to keep the heat pump running in mild conditions and only bring in the gas furnace during cold snaps. That reduces the number of abrupt mode changes and lets each source operate in its most stable range. But a poorly tuned hybrid—say, one that toggles between gas and electric every few minutes—will destroy repeatability faster than either source on its own. The real answer is that repeatability depends less on the fuel and more on modulation range and control strategy, with electric and well-tuned hybrid systems generally having the edge over basic gas.
Mold Cart Locking: Small Wear That Causes Big Wall Thickness Shifts
A mold cart that doesn't lock firmly can drift a few millimeters between cycles. Those tiny shifts transfer directly into the parison or preform alignment, and before long the wall thickness wanders from one side to the other. Operators often chase barrel temperatures or die gaps, but the real culprit is a worn latch sitting underneath the cart.
The wear usually starts with rounded corners on the locking pin or a stretched spring that no longer pulls the handle back. Because the movement is gradual, it rarely trips an alarm. However, even 0.5 mm of play at the cart translates into visible thickness variation in deep-draw or blow-molded parts, especially near pinch-off zones and bottom corners.
Checking the lock should be part of every shift handover. Push the cart side to side with the mold closed; if you feel a knock or see daylight between the latch faces, replace the pin and bushing as a set. A five-minute repair here prevents hours of sorting thin-walled rejects later.
Bearing Loads and Service Access: The Uptime Math Behind the Specs
Bearing load ratings rarely tell the whole story on their own. A spec sheet might list a dynamic load capacity that looks generous, but real uptime depends on how those loads fluctuate, spike during startups, or combine with misalignment and thermal growth. Equipment that runs close to its rated load for months at a time will degrade differently than a machine that sees sharp, intermittent overloads. The math behind uptime starts with a load spectrum, not a single number.
Service access changes that calculation in ways that are easy to overlook at the design stage. A bearing buried behind a coupling, guard, or structural member may be rated for the load, but if a technician needs four hours just to reach it, the effective downtime cost rises sharply. Smart layouts group high-wear bearings near access panels or leave enough clearance for a puller and torch. Even a modest gain in accessibility can cut replacement time by half, which matters more than a marginal increase in load rating.
When load ratings and service access are evaluated together, the uptime math becomes practical. You aren’t just checking whether a bearing can survive the applied forces; you’re calculating how long the whole repair cycle takes when it eventually needs attention. A slightly de-rated bearing that can be swapped in under an hour often outperforms a higher-rated unit that requires a crew, crane, and a full shift. That trade-off is where reliable machinery separates from impressive-looking data sheets.
FAQ
Stationary oven carousel machines keep molds moving through a fixed heating chamber, so every arm gets the same thermal exposure instead of relying on a moving oven that can drift. The carousel indexing is predictable, and once you dial in the cycle, you get repeatable wall thickness and fewer rejects on long runs.
Check whether the burners and airflow are laid out to create a truly balanced heat pattern across the full swing diameter. Look for adjustable burner zones and a well-insulated chamber that recovers quickly after the door opens. The best designs also position the mold arms so the mold itself rotates through multiple air layers rather than sitting in a single temperature band.
Arm diameter sets your mold envelope and how many stations you can run at once. Going too large with small molds wastes energy and floor space, while a tight diameter can limit you on larger tanks or playground components. Match the swing diameter to your largest realistic mold plus clearance so you don't end up with a machine that can't grow with your product line.
Keep an eye on the carousel drive gear and arm bearings since they take the brunt of the loading. Grease fittings on a schedule, check chain or gear tension monthly, and inspect oven seals and burner nozzles for soot buildup that changes heat output. Most unexpected downtime comes from neglected small parts, not major failures.
Yes, but you need to pay attention to the secondary axis rotation and speed ratio. A well-tuned carousel machine lets you adjust the arm rotation independently from the plate rotation, which helps powder reach deep pockets and corners. For parts with long narrow channels, you might slow the secondary rotation and use a drop box or internal air to build thickness where it matters.
Stationary carousel ovens usually have better fuel efficiency because the chamber holds heat and the part isn't exposed to open flame, which can scorch material if you push too hard. Cycle times can be a bit longer than a direct-fired rock-and-roll on thin-walled parts, but you gain on thicker parts and engineering resins because the slower, more even heat soak reduces warpage and post-mold cooling time.
Look for interlocks that stop burner operation if the oven door opens unexpectedly, emergency stops at every operator station, and flame-safety systems that shut off fuel if ignition fails. Thermal relief on the chamber and guarding around the rotating arms prevent operator contact with hot metal. Also check that the control panel gives clear fault codes instead of just an alarm light.
Tank and container manufacturers, automotive fluid reservoirs, agricultural chemical tanks, medical carts, and large playground or outdoor furniture producers. These segments usually run medium to large parts that benefit from the machine's consistent heating and ability to handle multi-cavity molds without the part-to-part variation you see on smaller shuttle systems.
Conclusion
Reliable rotomolding output depends less on chasing a single peak temperature and more on how evenly the oven delivers heat across every mold surface. Proper airflow distribution prevents hot spots and cold zones that quietly distort wall thickness, while independent arm drives let each mold rotate at its own optimal speed instead of forcing a compromise. This flexibility shortens cycle times in real production, not just on paper, and it reduces the temptation to pull parts early—a habit that locks residual stress into the plastic and leads to warpage or premature cracking once the part cools.
Choosing between gas, electric, or hybrid heat is not about raw energy cost alone; it is about repeatability from one cycle to the next. Electric elements respond quickly and hold a tight band, gas can be cheaper but swings more with ambient conditions, and hybrid setups aim for a balance. Meanwhile, small wear in mold cart locking mechanisms often goes unnoticed until wall thickness starts drifting, and bearing loads that look fine on a spec sheet create downtime if service access is poor. For a stationary oven carousel machine to stay dependable, the design must make maintenance straightforward rather than treating uptime as an afterthought.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com