OEM High-Pressure Forged Steel Valve Factory: Key Considerations for Durable Valve Sourcing
2026-10-16
High-pressure systems don’t forgive weak points. A forged steel valve that fails under extreme conditions isn’t just a part replacement—it’s a shutdown, a safety risk, and a budget drain. So when you’re evaluating OEM valve factories, the usual checklist won’t cut it. Durability here depends on details most buyers overlook. ZMV has spent years refining those details, and this guide walks through what actually matters.
The Forging Difference You Can Actually Feel
Most knives feel like tools; a forged blade feels like an extension of your hand. The extra density from hammering aligns the steel's grain structure, so the balance point sits naturally where your index finger meets the bolster. You notice it the first time you lift it—there's a quiet heft that isn't about being heavy, but about being grounded.
Run your thumb along the spine and you'll feel the subtle taper that only comes from repeated heating and shaping. Forged edges don't fight the material; they move through with a controlled, almost silent glide. The difference shows up in the way a cut starts clean and finishes clean, without the micro-wobble you get from thinner stamped blades.
Over weeks of daily use, that initial impression deepens. The edge holds its bite longer because the forging process packs the steel tighter and eliminates internal weaknesses. When you sharpen it, the burr forms evenly and wipes away with fewer strokes. That's the part most people can't articulate but immediately recognize—a blade that still feels new after the honeymoon is over.
Why Wall Thickness Isn't Just a Number
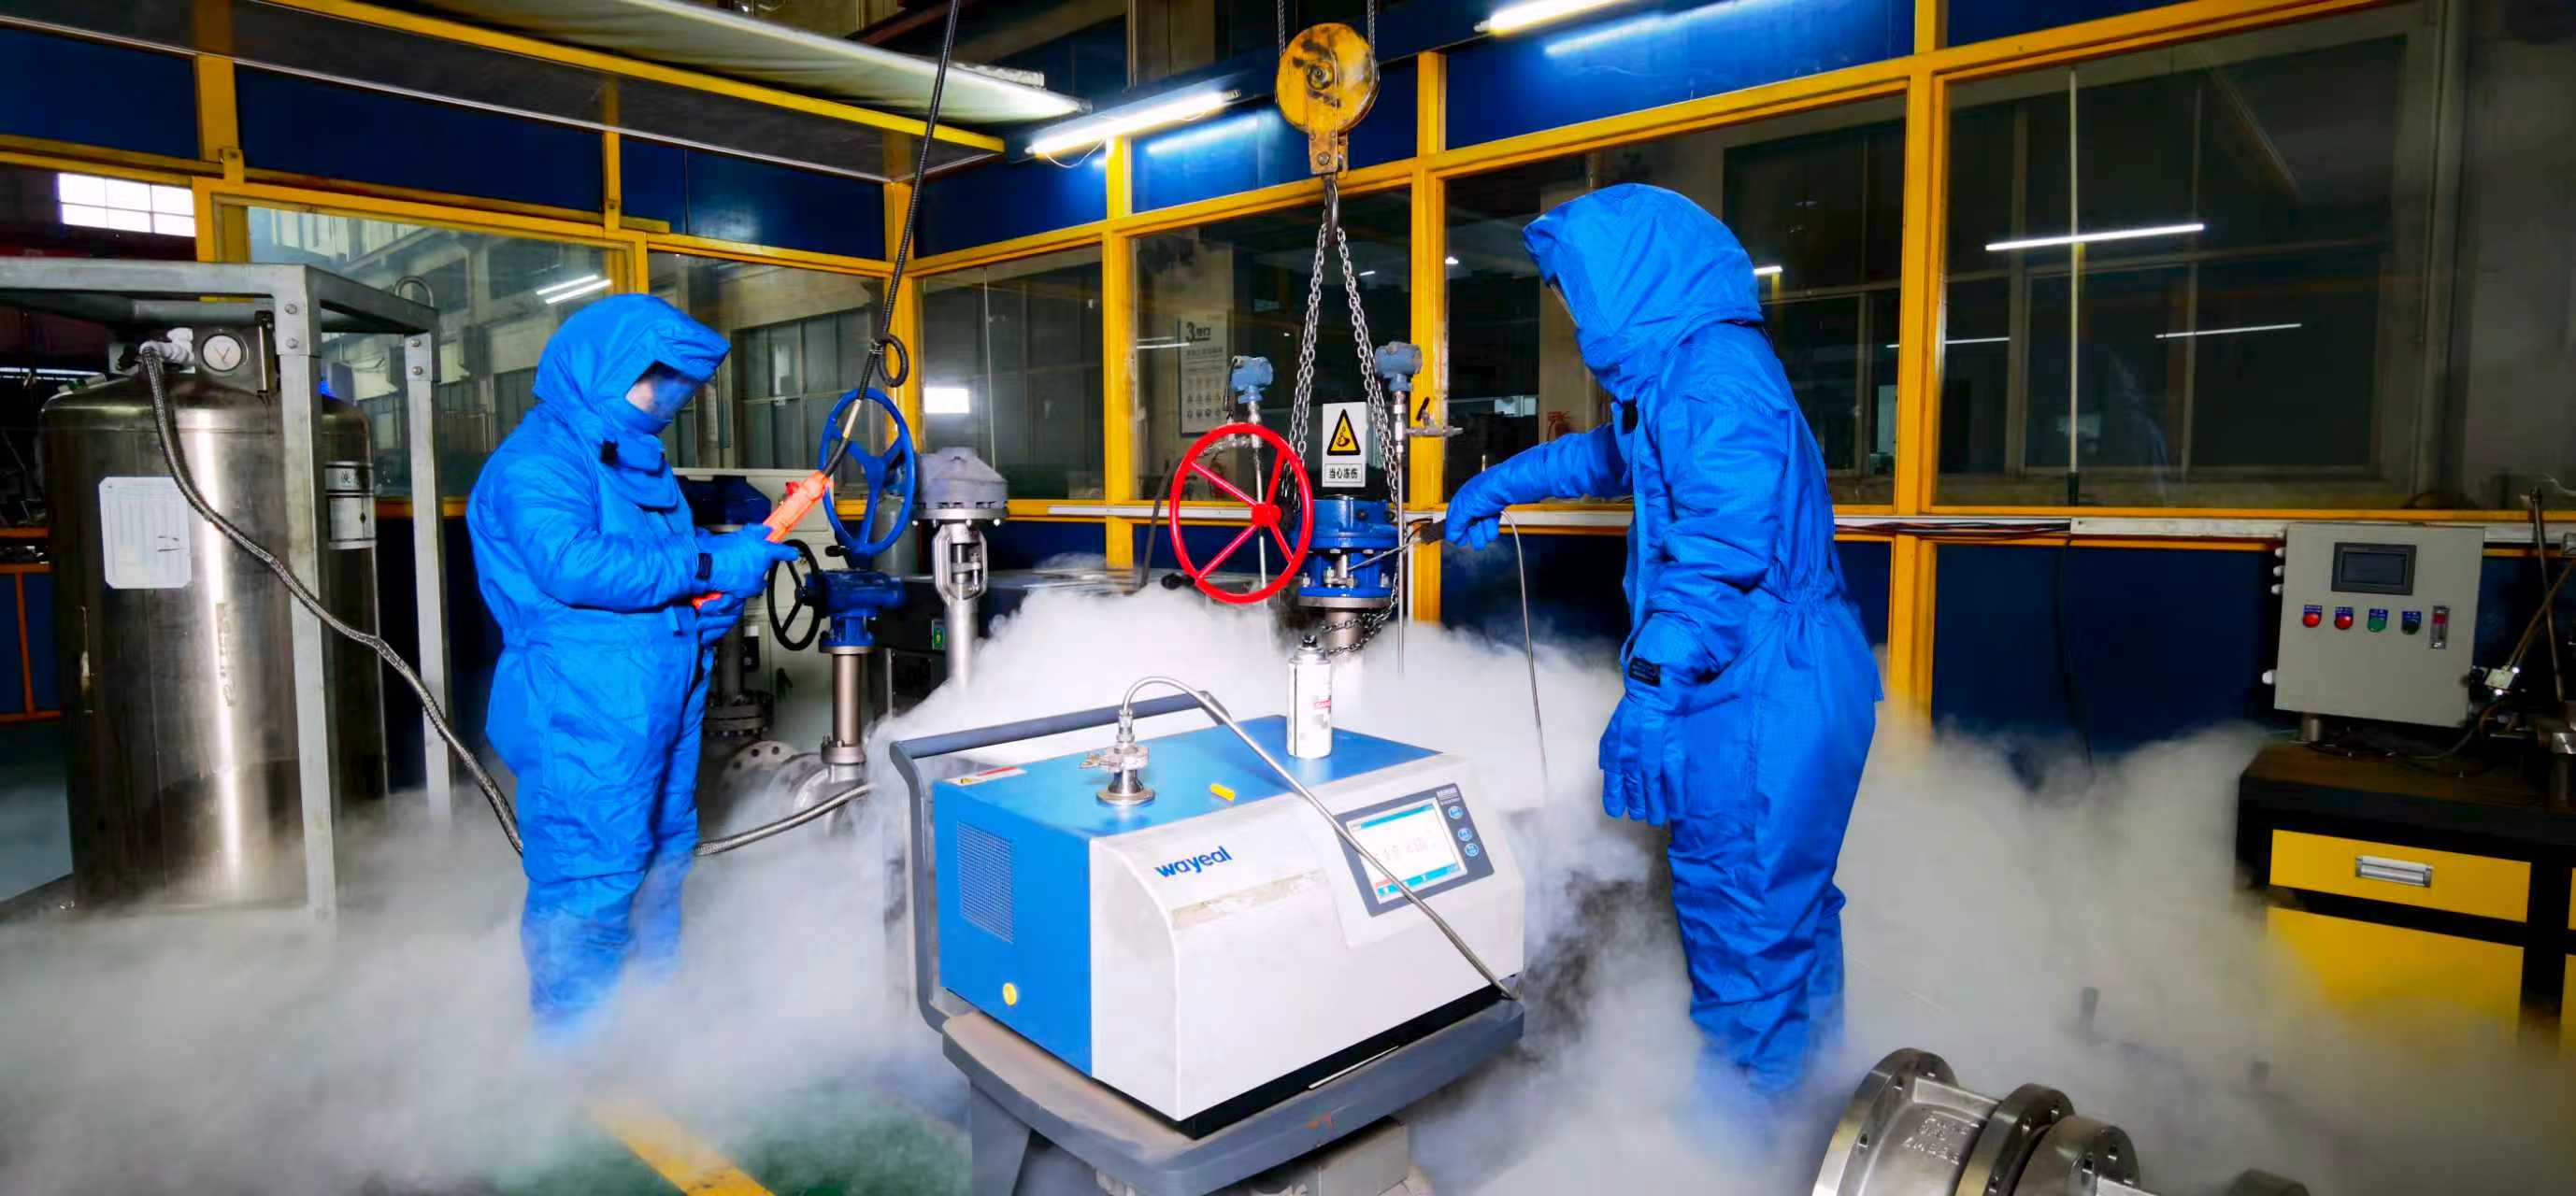
When engineers glance at a drawing, wall thickness often reads as a single line item—just another dimension to plug into a CAD model. But on the shop floor or in the field, that number quietly dictates how a part withstands pressure, handles thermal cycling, and survives years of abuse. A 3 mm wall in one polymer might flex like a credit card, while the same dimension in a glass-filled nylon could crack under the same load. The raw value means little until you know the material's elongation, notch sensitivity, and creep behavior.
Manufacturing adds another layer of complexity. Injection molding a thick boss next to a thin rib creates differential cooling, which warps the part or leaves sink marks that ruin surface finish. Welders know that a 6 mm pipe wall behaves very differently than a 10 mm wall when it comes to heat input and distortion, even though the pressure rating might only shift by a few bar. These effects don't show up in a simple spreadsheet calculation; they emerge from how the material freezes, shrinks, or resists localized stress.
Then there's the cost and weight tug-of-war. Trimming a millimeter from a bracket might save 15% in material, but it can also lower the natural frequency enough to invite resonance from a nearby motor. In pressure vessels, a thicker wall adds safety margin against corrosion, yet it also raises thermal gradients during startup, which can drive fatigue cracks. Good designers treat wall thickness as a dial that tunes stiffness, damping, and manufacturability all at once—not as a standalone entry on a spec sheet.
Seats and Seals: The Real Cost of Cutting Corners
The logic of choosing cheap seats and seals seems irresistible at the purchase order. A few cents saved on an O-ring or a pound of lower-grade elastomer looks like an easy win against a tight budget. But seats and seals are not passive components; they are the front line against pressure loss, contamination, and uncontrolled flow. When a seat begins to erode or a seal takes a compression set, the damage rarely stays contained. Leakage becomes a slow bleed that erodes efficiency long before anyone notices, and by the time a failure is visible, the downstream costs have already started piling up.
What often gets left out of the initial cost comparison is the price of unplanned intervention. A failed pump seal in a chilled water loop can shut down an entire building floor. A scored valve seat in a chemical transfer line forces a line break, purge, and re-qualification. Each event carries labor, lost production, and sometimes regulatory exposure that dwarfs the difference between a commodity part and a properly specified one. In hydraulic systems, a single hard particle passing a worn seal can take out a cylinder rod, a servo valve, and a pump in sequence. The original 'saving' becomes a rounding error against the repair invoice.
The real cost of cutting corners on seats and seals is not measured at the vendor's counter but in the operating calendar. Quality components are matched to the actual service conditions—temperature swings, chemical compatibility, pressure spikes, and cycle rates. They are machined to hold tolerances and installed without shortcuts. This does not mean spec overkill; it means refusing to gamble on failure modes that are well understood. When seats and seals are treated as engineered parts rather than commodities, the payback shows up as longer intervals between shutdowns, cleaner fluid, lower energy consumption, and far fewer midnight phone calls.
Reading Mill Test Reports Without a Translator
Mill test reports pack a lot of information into a small space, but you don't need a metallurgist or a language expert to make sense of them. Start by scanning for the heat number and the material specification—these two alone tell you whether the steel matches what your project calls for. The chemical composition table is next: look for carbon, manganese, phosphorus, and sulfur first, since these affect weldability and strength the most. If the numbers fall within the limits listed in the spec, you're usually in good shape.
Mechanical properties can trip people up because they use abbreviations like YS, TS, and EL. YS means yield strength, TS is tensile strength, and EL stands for elongation. You don't need to memorize every term—just compare the reported values against the minimums on your purchase order. A quick trick is to highlight any value that's lower than the requirement; that's often the first sign a heat might not be acceptable.
Finally, pay attention to the signature and date at the bottom. A valid mill test report should be traceable to the original producer, not just a distributor's stamp. If the document looks photocopied or the heat number doesn't match the physical marking on the material, stop and ask for clarification. Reading these reports gets faster with practice, and after a few dozen you'll start spotting non-conformances without breaking stride.
Factory Audits That Go Beyond the Conference Room
Most audit reports start and end in a meeting room, with binders full of checklists and a polite nod before everyone files out. That’s not how we work. Our factory audits are built on walking the floor, talking to line operators, checking raw material storage, and observing how equipment is actually maintained between shifts. We spend more time beside the conveyor belts and loading docks than at a conference table, because that’s where the real story of a factory comes out—the one that won’t show up in a PowerPoint deck.
We don’t rely on pre-submitted documents or sanitized sample areas. Instead, we follow the product backwards from the finished carton to the incoming material, tracing every touchpoint. Our auditors open random crates, measure tool wear on the spot, and ask workers questions that aren’t on any form. If a machine has a handwritten repair log taped to its side, we read it. If the night shift leaves different notes than the day shift, we notice. These are the details that separate a paper-passing factory from one that actually controls its process.
The result is an audit report that reads less like a compliance scorecard and more like a physical walkthrough of what we saw, heard, and measured. No generic “needs improvement” boxes. We give you specific photos of the exact rust spot, the pallet stacking pattern, the calibration sticker that expired three weeks ago. And when we leave, you know not just whether the factory meets a standard, but whether it can keep meeting it six months from now when nobody’s watching.
Custom Valve Orders Without the Guesswork
Every custom valve order starts with a simple conversation about your exact operating conditions. Instead of forcing you to browse through generic catalogs, we gather details like pressure ratings, media compatibility, and connection types upfront. This eliminates the back-and-forth that usually comes with made-to-order components, so what you receive matches what you actually need.
Our engineering team uses the specifications you provide to create a clear proposal, including dimensional drawings and material options. You’ll never have to guess whether a seat material will hold up to your temperature range or if the actuator sizing is correct. Everything is verified before production begins, which means fewer surprises when the valve arrives on site.
Even after delivery, the order details stay on file. If you need a repeat order or a slight modification, we can pull up the original configuration and make precise adjustments without restarting the whole process. That’s how custom valve sourcing should work—practical, transparent, and free of guesswork.
FAQ
Go beyond brochures and ask to see the actual forging line, heat treatment furnaces, and pressure testing stations. A factory that controls these steps in-house can respond faster to material deviations and holds tighter tolerances than one relying on subcontracted work.
Ask for full traceability from the heat number to the final pressure test chart. Look for factories that perform grain flow analysis on sample forgings, because proper grain orientation around the body and bonnet is what prevents fatigue cracks in cyclic high-pressure duty.
A105 is common but often over-specified. For sour gas or chloride exposure, consider F316 or duplex stainless, and make sure the factory can document actual mechanical properties after heat treatment—not just nominal values from the grade.
Overlooking the seat and stem material pairing. The body may be a robust forging, but if the trim is a soft seal rated below the operating temperature, the valve will leak long before the body shows wear. Specify hard-faced seats and live-loaded packing for cyclic service.
Request records of actual NDT procedures—ultrasonic or magnetic particle—on forgings before machining. A strong indicator is a factory that rejects its own material when indications are ambiguous, rather than pushing borderline parts through to meet a shipment date.
Differences hide in requirements like full penetration welds, post-weld heat treatment, and pressure test durations. A cheaper quote often trims these steps, which shortens initial savings but creates leak paths or stress corrosion risks later.
At minimum, shell and seat hydrostatic tests, plus a low-pressure air seat test. For critical service, add nitrogen leak testing and a production sample burst test to confirm the actual safety margin of the forging design.
Ask for a design review meeting with their engineers and request a failure mode analysis for your specific pressure and temperature range. A capable factory will point out potential cavitation, thermal shock, or gasket compatibility issues instead of simply confirming they can make the part.
Conclusion
You don't need a micrometer to tell when a forged valve body has been worked properly. The grain structure follows the shape, and the metal feels dense in a way that castings simply don't. When you spec an OEM high-pressure valve, pay attention to that difference first, because it sets the baseline for everything else. Wall thickness is another thing that gets quietly reduced on drawings. A valve can meet the flange dimensions and still have a body wall that's barely above the pressure calculation cutoff. Ask for sectional drawings and check the minimum wall at the valve's thinnest point, not just the average. Seats and seals are where suppliers often shave cost. Substituting a lower-grade PEEK or a softer PTFE blend might pass a short hydro test, but it will cut into the valve's cycle life once abrasive media or temperature swings show up. When mill test reports arrive, don't just file them. Read the heat numbers, trace the chemical composition back to the melt, and confirm the tensile and yield values actually match what you ordered. A report that simply says conforms without listing numbers is a flag.
A real factory audit doesn't end in the conference room. Walk the floor and watch how they handle preheating before weld overlay, how they calibrate test benches, and whether pressure testing is done with calibrated gauges or just a shop air line. Custom valve orders fail most often because someone assumed a standard dimension would work. Don't leave the guesswork to the supplier. Send complete data sheets, mark up your own drawings, and specify end connections, pressure classes, actuation torque, and any coating or NDE requirements. A good OEM factory will come back with questions about service conditions, not just a price. They'll ask about flow direction, frequency of operation, and what's actually flowing through the valve. Those questions are the difference between a supplier that builds to a spec and one that builds to your actual service. Sourcing durable high-pressure forged valves isn't about finding the cheapest quote; it's about matching the physical evidence from the forge, the material traceability, and the factory's testing habits to the demands of your system.
Contact Us
Contact Person: Lucas Lin
Email: [email protected]
Tel/WhatsApp: +8613968913000 / +8613868610141
Website: https://www.zhengmaogroup.com