Aluminum Fishing Boat Manufacturer Shares Top Design Secrets for a Stable and Durable Hull
2026-09-22
Every angler knows the moment a hull stops feeling like a liability and starts feeling like an extension of your instincts. That shift doesn't happen by accident. It comes from deliberate design choices—especially in aluminum fishing boats, where the right construction means the difference between a dry, stable platform and a hull that shudders in chop. Here, the team at Allheart shares the design secrets behind their most stable and durable hulls, from plate thickness and rib spacing to chine geometry. Read on to learn what separates a boat built for decades from one that just looks good at the dock.
Chine Geometry: The Overlooked Key to a Stable Ride
Most riders fixate on head angle, trail, or wheelbase when chasing stability, but the chine—the distinct crease running along the lower edge of the frame or hull—quietly shapes how a vehicle settles into a turn. A deeper, sharper chine gives the structure a predictable bite in corners, resisting wallow without making the steering feel heavy. Ignore it and you end up compensating with extra damping or tire pressure, masking the real issue.
Chine placement also determines how weight transfers during acceleration and braking. Move it too far forward and the rear feels loose under hard throttle; too far back and the front pushes wide. The best setups treat the chine as a dynamic reference line, not just a styling crease. Subtle changes of a few millimeters can transform a nervous chassis into one that tracks straight with minimal input.
On rough surfaces, chine geometry controls how energy travels through the structure. A rounded or softly blended chine spreads impacts over a larger area, reducing sharp feedback but sacrificing some precision. A crisper edge channels forces along a defined path, letting the suspension do its job without fighting hidden flex. That balance between comfort and control is why experienced builders keep returning to this overlooked dimension.
Why We Put More Aluminum in the Keel Than the Sides
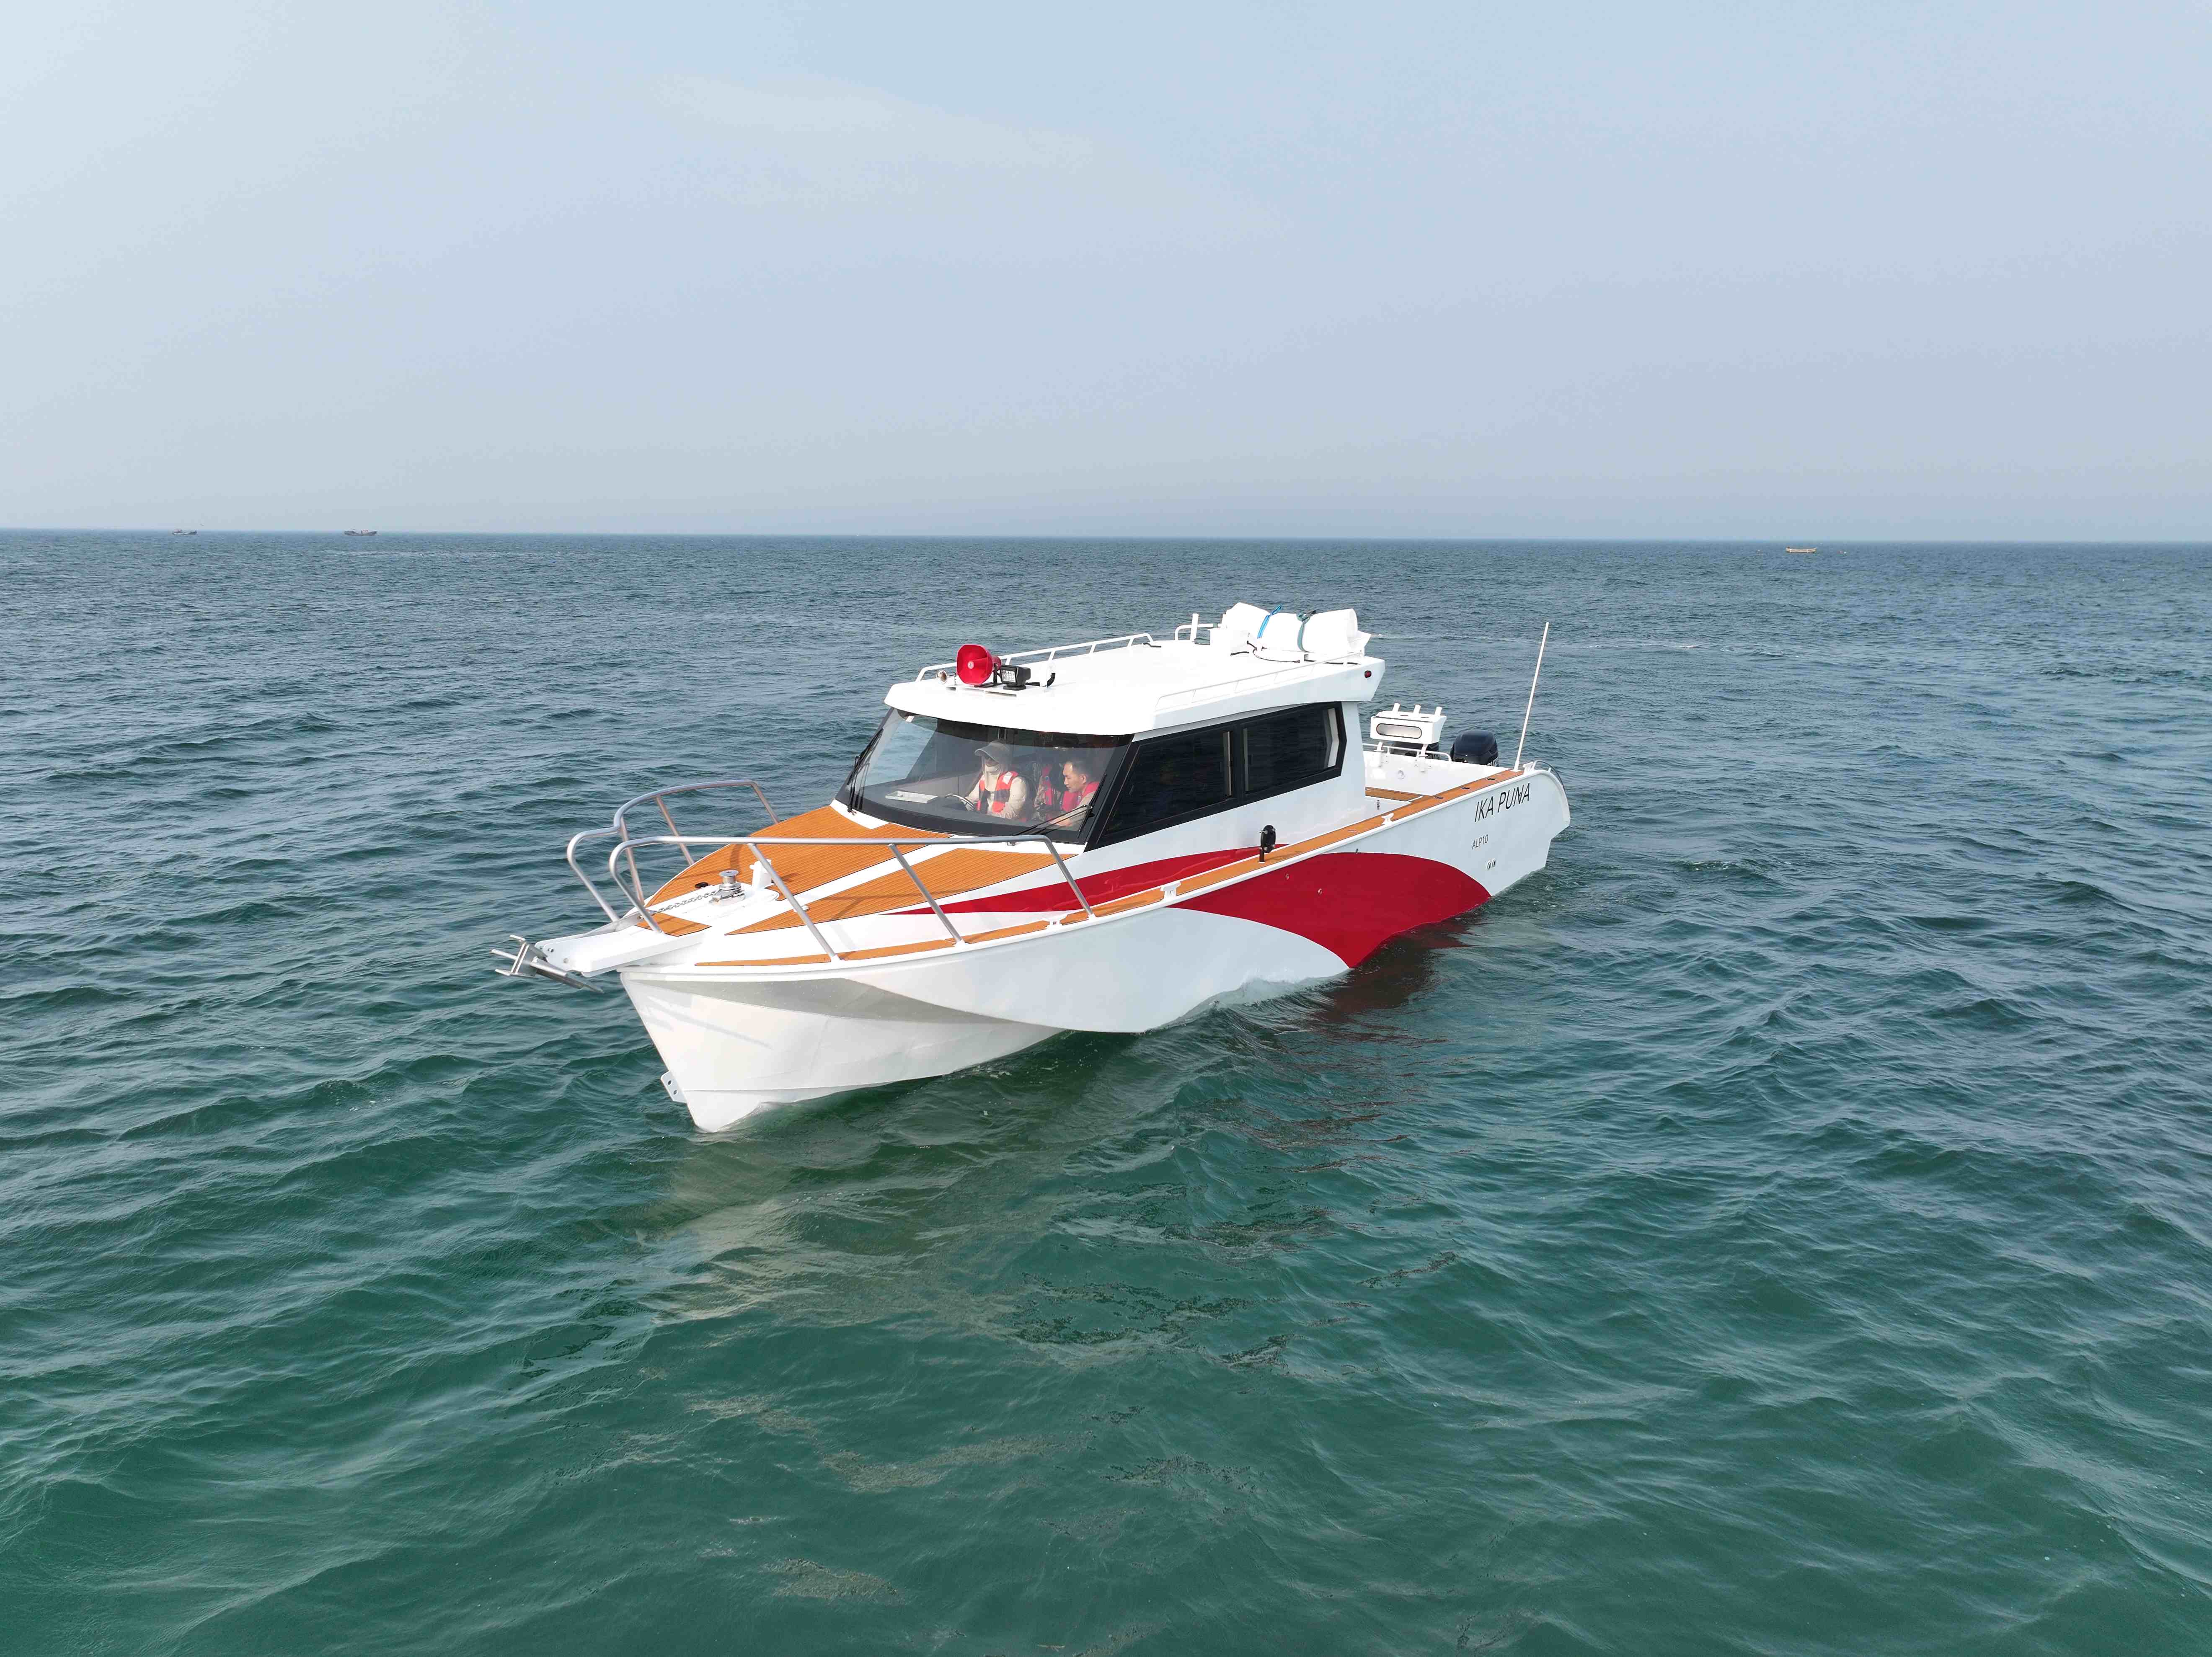
On most aluminum boats, the keel is the primary load path. It runs the full length of the hull and ties the stem to the transom, so every wave impact and torsional load passes through it. Thickening the aluminum here resists fatigue cracks and dents from grounding or trailer rollers. The sides don't carry nearly as much stress; they are essentially curved panels that need to hold their shape and keep water out. Adding thickness to them would increase weight and material cost without any meaningful gain in durability.
We also have to consider how frames and bulkheads attach. A heavier keel section gives the welders a solid, stable base to tie into, which reduces distortion and weld cracking over time. If the keel were as thin as the side plating, those joints would flex more and start failing at the edges. By putting extra aluminum in the keel, the whole structure stays aligned under load, while the sides can be formed from lighter sheet that is easier to bend into compound curves.
In addition, the keel lives in a tougher environment. It scrapes over rocks, sandbars, and ramps far more often than the upper side plating. That extra thickness acts as a wear allowance, extending the hull's useful life before repairs are needed. The trade-off is minimal because any weight added low and on centerline actually lowers the boat's center of gravity, which often improves stability. The sides stay light, which helps with planing, fuel burn, and overall handling.
Welding Methods That Prevent Stress Cracks Over Time
Stress cracks in welds often develop when the metal cools unevenly or hydrogen gets trapped in the joint. One of the most reliable ways to avoid this is to preheat the base material before striking an arc. A steady, controlled preheat reduces the temperature difference between the weld pool and the surrounding metal, which lowers the cooling rate and gives hydrogen a chance to escape. For thicker sections or high-carbon steels, maintaining an interpass temperature can make the difference between a weld that lasts decades and one that needs repair within a year.
Post-weld heat treatment is another safeguard that is frequently overlooked. By holding the finished weld at a moderate temperature for a set period, residual stresses locked into the joint are allowed to relax gradually. This step is especially useful for large fabrications or components that will experience cyclic loading. It does add time and cost, but the alternative—chasing cracks after the part is in service—is far more expensive.
Choosing the right filler metal also plays a bigger role than many welders expect. A filler with slightly lower strength but higher ductility can absorb shrinkage stress without tearing. Low-hydrogen electrodes or wire, combined with proper storage and handling, prevent moisture from introducing hydrogen into the weld. When paired with controlled heat input and a consistent travel speed, these choices produce a joint that resists stress cracks over time instead of simply hiding them until the next inspection.
The Real Difference Between 5052 and 5086 Alloy
If you have ever held a piece of 5052 and a piece of 5086 side by side, the difference is not obvious at first. Both belong to the 5000 series, both resist corrosion, and both weld without much fuss. But the alloy recipes diverge in ways that matter once you bend, weld, or leave them in salt spray. 5052 relies on chromium as its main grain-control addition, with magnesium around 2.5 percent. 5086 pushes magnesium closer to 4 percent and replaces most of that chromium with manganese. That shift changes how the metal strain-hardens during forming and how much strength it keeps after welding.
In practical terms, 5086 typically delivers higher tensile and yield strength in comparable tempers, which is why it shows up in hull plates, pressure vessels, and other welded structures. It also holds up a bit better in seawater and resists stress corrosion cracking near welds more consistently. 5052 remains the easier alloy to form into deep or complex shapes, and it is usually cheaper and more widely available. If your job involves severe bending or drawing, 5052 is the more forgiving choice; if it involves a welded assembly under load in a marine environment, 5086 justifies the extra cost.
None of this makes one alloy universally superior. The real difference comes down to how each one behaves after fabrication: 5086's manganese-magnesium balance keeps more strength around weld zones and tolerates prolonged salt exposure with less pitting, while 5052's chromium-based chemistry favors ductility and smoother forming. Pick based on the loads and environment, not just the spec sheet.
How Transom Design Affects Trolling and Planing
The way a transom meets the water has a direct but often overlooked effect on how a boat behaves at trolling speeds. A wide, slightly raked transom spreads buoyancy across the stern, keeping the aft end from squatting too deeply when the engine is idled down. That shallow stern draft keeps lures running at their intended depth instead of pulling them into a nose-high, tail-down posture. In contrast, a narrow or sharply angled transom allows the stern to settle, which increases wetted surface and drag—subtle at first, but enough to raise fuel burn over a long day of slow trolling.
Once the throttle goes down and the hull climbs onto plane, transom shape dictates how cleanly water releases from the bottom. A transom with a crisp lower edge or a notched pad lets the flow separate without clinging to the hull, which reduces drag and helps the boat reach planing speed sooner. Transom height also matters here: too tall for the outboard and the prop may start to ventilate in chop; too low and the lower unit digs in, creating spray and slowing acceleration. Some builders integrate slight steps or angled setbacks into the transom to fine-tune that transition.
Openings and hardware mounted on the transom—livewell drains, transducer brackets, boarding ladders—can disturb the water flowing past the stern in ways that affect both modes. At trolling speeds, a poorly placed drain may create a small eddy that tugs at fishing lines. At planing speeds, that same disturbance can become a source of spray or ventilation. The best transom designs treat the whole surface as a functional part of the running bottom, not just a mounting board for the engine.
Tested in Chop: What Our Hulls Learn from Rough Water
Rough water has a way of exposing every shortcut. When we run hulls through short, steep chop, the real feedback comes from the places that start to protest—weld seams under the bow flare, the transition where the deadrise flattens out, the chine that catches instead of sheds. Those stress marks are the first draft of the next revision.
What a hull learns in those conditions doesn't come from a simulation. It comes from watching gelcoat crack patterns after repeated slamming, from measuring how much the transom twists when a following sea shoves the stern sideways. We found that moving the entry angle just two degrees changed the impact signature entirely—less vertical acceleration, less spray thrown over the shoulder, less fatigue on the steering gear.
Some builders chase calm-water numbers. We'd rather see a hull come back from a messy afternoon with salt crust in the scuppers and a list of small failures to correct. Each one teaches us something about how water actually loads a structure in motion. The result is a boat that feels less like it's fighting the sea and more like it's using the roughness to stay settled.
FAQ
We use a modified V with a wider beam and a flatter deadrise at the stern. That combination gives you the stability of a flat-bottomed boat when you're standing and casting, but the sharper entry forward still slices through chop instead of slamming.
5086 has better corrosion resistance in saltwater and higher tensile strength, so we can use slightly thinner plate without sacrificing toughness. That keeps the hull light enough to plane efficiently but still stiff enough to resist flexing under load.
We avoid hard corners by using rolled or extruded sections with generous radii, and we weld in a sequence that reduces heat distortion. The ribs are also spaced closer together in high-stress areas like the bow and transom, so the metal doesn't work-harden as quickly.
We add a full-length external keel strip made of a harder 6061-T6 alloy. It acts as a sacrificial wear bar, taking the abrasion from sand and gravel. When it eventually wears down, you can replace that strip instead of rebuilding the entire bottom.
Some of our offshore models use a sealed double bottom with closed-cell foam between the skins. It adds buoyancy, deadens sound, and gives a second barrier if the outer hull is punctured. The trade-off is extra weight, so we only use it on larger boats that can carry it.
We run prototypes through a mix of controlled stress tests and on-water torture runs, including repeated hard landings in rough water and loading the deck beyond its rated capacity. We also cut apart early hulls after testing to inspect for hidden stress cracks at the weld toes.
Rinse with fresh water after saltwater use, especially inside the bilge where salt can sit against bare metal. Check the sacrificial anodes twice a year, and repair any deep scratches in the paint or mill scale promptly. Never use copper-based antifouling paint directly on aluminum.
Conclusion
A stable, durable aluminum fishing hull doesn't come from a single flashy feature—it's the quiet details that earn trust over years of hard use. One of the most overlooked is chine geometry. We shape the reverse chines to direct spray outward and down, which not only keeps the boat dry but also lets it track predictably in a crosswind. That predictability matters when you're fighting a fish on one side and the wind is pushing from the other. We also deliberately put more aluminum in the keel than the sides, not because it looks better on a spec sheet, but because that's where the hull takes the biggest beating—from trailer rollers, rocky launches, and the occasional accidental grounding. The keel is the backbone; if it flexes too much, every rivet and weld downstream starts working loose.
Welding methods are another area where patience pays off. We avoid full-length continuous welds in high-stress areas, instead using intermittent stitch welding with controlled heat input. This lets the aluminum expand and contract without building residual stress that leads to cracks years later. And not all aluminum is created equal—we run 5086 alloy on the bottom and sides because its higher magnesium content resists saltwater corrosion better than 5052, which we reserve for interior bracing and decks. The transom gets special attention too: a slight angle change can make the difference between trolling smooth and porpoising at mid-throttle. We've spent days in rough chop, not just to see if the hull survives, but to learn where water pressure builds and where it needs more support. That's the kind of testing you can't fake in a showroom.
Contact Us
Contact Person: Benny Hu
Email: [email protected]
Tel/WhatsApp: +8618354225697
Website: https://www.allheartmarine.com/